

[What is High-Calcium Powder Conveying Equipment? And What Are Its Design Principles?]
High-calcium powder conveying equipment is a specialized system designed to handle and transport high-calcium powder materials efficiently. This equipment is crucial in industries such as food processing, pharmaceuticals, and chemical manufacturing, where precise and reliable powder handling is essential for maintaining product quality and operational safety. The design of these systems is tailored to address the unique challenges posed by high-calcium powders, including their density, flow characteristics, and potential for dust generation.

Understanding High-Calcium Powder Conveying Equipment
High-calcium powder conveying equipment, as the name suggests, is engineered to manage the transportation of powders that contain a high proportion of calcium compounds. These powders are often used in applications like calcium supplement production, dairy processing, and industrial chemical synthesis. The primary goal of such equipment is to ensure that the powder is moved from one location to another without degradation, contamination, or loss. This involves controlling factors like particle size, moisture content, and the risk of agglomeration or caking, which can affect the powder's flowability and overall performance.
The Core Components and Design Principles
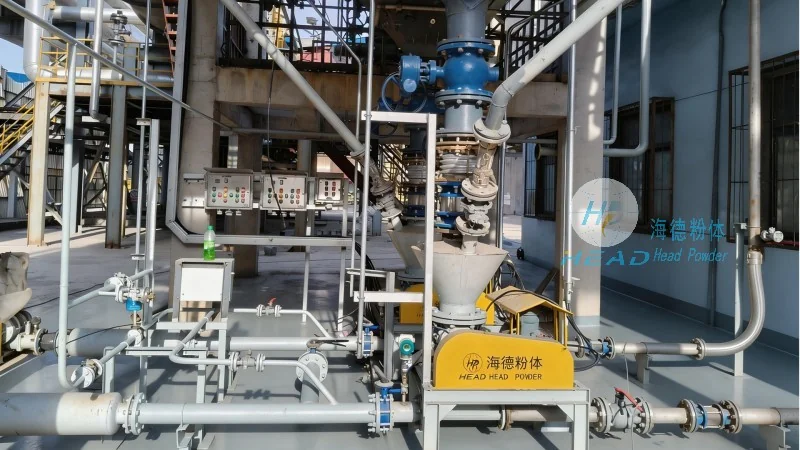
The design of high-calcium powder conveying equipment typically revolves around several key components that work in tandem to achieve efficient and safe powder handling. These components include feeders, conveyors, and control systems, each designed to address specific aspects of the powder's behavior. For instance, feeders are often used to regulate the flow rate of the powder, ensuring a consistent and controlled feed to the conveyor system. This is particularly important for high-calcium powders, which can be prone to bridging or uneven flow if not managed properly.

Conveyor systems, such as pneumatic or mechanical conveyors, are commonly employed to transport the powder. Pneumatic conveyors use air pressure to move the powder through a pipeline, while mechanical conveyors rely on physical components like belts or screws. The choice of conveyor type depends on the powder's characteristics, such as its density and moisture content, as well as the distance and layout of the conveying path. In the case of high-calcium powders, pneumatic conveyors are often preferred due to their ability to handle fine powders and minimize dust exposure.
Key Design Considerations for High-Calcium Powder Handling
When designing high-calcium powder conveying equipment, several critical factors must be considered to ensure optimal performance and safety. One of the most important considerations is the prevention of dust accumulation and explosion hazards. High-calcium powders can be combustible when mixed with air, and therefore, equipment must be designed with explosion-proof features and effective dust collection systems. This includes the use of sealed containers, proper ventilation, and regular maintenance to prevent dust buildup.
Another key design consideration is the control of moisture content. High-calcium powders are often hygroscopic, meaning they can absorb moisture from the air, leading to caking or clumping. To mitigate this, the conveying equipment may include drying or dehumidification components, such as desiccant filters or heated sections, to maintain the powder's flowability. Additionally, the equipment's materials of construction are chosen to be compatible with the powder, avoiding reactions that could alter the powder's properties or cause corrosion.
Applications and Benefits of High-Calcium Powder Conveying Equipment
High-calcium powder conveying equipment is widely used in various industries, offering several benefits that enhance operational efficiency and product quality. In the food industry, for example, such equipment is used to transport calcium supplements, dairy powders, and other nutritional additives. The precise control over powder flow and handling ensures that the final products meet strict quality standards and regulatory requirements. Similarly, in the pharmaceutical industry, high-calcium powder conveying systems are used to transport raw materials for calcium-based medications, ensuring that the powders are handled in a sterile and controlled environment.

In the chemical industry, high-calcium powder conveying equipment is employed in the production of calcium-based chemicals, such as calcium carbonate and calcium chloride. The ability to handle these powders efficiently and safely is crucial for maintaining production rates and minimizing downtime. The equipment's design also contributes to cost savings by reducing material waste and improving overall process efficiency. By ensuring that the powder is transported without degradation or loss, the equipment helps to maintain the purity and quality of the final products, which is essential for meeting customer and regulatory expectations.
Conclusion
High-calcium powder conveying equipment is a sophisticated system that combines advanced engineering and material science to handle the unique challenges of high-calcium powders. The design principles, components, and considerations discussed above highlight the importance of precision, safety, and efficiency in these systems. As industries continue to rely on high-calcium powders for various applications, the development of advanced conveying equipment will remain critical in ensuring that these materials are handled effectively and responsibly. Companies like Shandong HeadPowder Engineering Co., Ltd., based in China, play a vital role in providing such equipment, leveraging their expertise to meet the diverse needs of their clients in the food, pharmaceutical, and chemical sectors.