

What is a Rare Earth Crystal Powder Material Pneumatic Conveying System? What are its Design Princip
For industrial applications involving the handling of rare earth crystal powders, efficient and reliable material transport is crucial. A rare earth crystal powder material pneumatic conveying system is a specialized solution designed to move these fine, often abrasive, powders through a pipeline using air or other gas as the conveying medium. This system is particularly important in industries such as rare earth processing, where the integrity and purity of the material must be maintained during transport.

Understanding the Core Components of the System
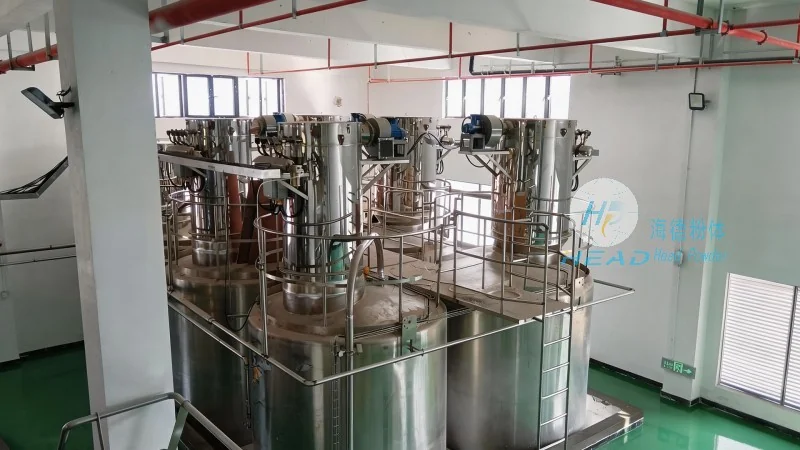
The pneumatic conveying system for rare earth crystal powders typically consists of several key components that work in tandem to ensure effective material transfer. These components include the material feed hopper, which holds the powder and controls the flow rate; the conveying line, which is the pipeline through which the powder travels; the air or gas source, which provides the necessary pressure or velocity to move the material; and the control system, which regulates the operation of the entire system. Each component is designed to handle the unique properties of rare earth crystal powders, such as their fine particle size and potential for static charge accumulation.

Design Principles for Efficient Material Handling
The design of a rare earth crystal powder pneumatic conveying system is based on several fundamental principles to ensure optimal performance and material integrity. One key principle is the selection of appropriate air velocity and pressure to achieve the desired conveying rate without causing excessive particle breakage or degradation. The system must also account for the potential for particle agglomeration or caking, which can affect flow characteristics. Additionally, the design considers the need for proper filtration and separation to prevent dust accumulation and maintain the purity of the conveyed material. The control system plays a critical role in adjusting these parameters in real-time, ensuring consistent performance under varying operating conditions.

HeadPowder's Expertise in Pneumatic Conveying Solutions
Shandong HeadPowder Engineering Co., Ltd., commonly known as headpowder, is a leading provider of specialized pneumatic conveying systems tailored for rare earth crystal powders. With a focus on engineering excellence and customer-specific solutions, headpowder designs and manufactures systems that meet the unique requirements of rare earth processing facilities. The company's expertise lies in understanding the material properties of rare earth powders and translating that knowledge into robust, efficient, and reliable conveying systems. By leveraging advanced engineering principles and materials, headpowder ensures that its systems can handle the challenges associated with rare earth crystal powder handling, including high dust content, abrasive wear, and static electricity.
Key Features and Advantages of the System
The rare earth crystal powder pneumatic conveying system offers several advantages over traditional bulk material handling methods. One of the primary benefits is the ability to transport materials in a closed system, which reduces dust emissions and improves workplace safety. This is particularly important for rare earth powders, which can be hazardous if inhaled. Additionally, the system allows for precise control over material flow rates and pressure, enabling accurate dosing and processing. The closed pipeline design also helps maintain the purity of the material by preventing contamination from external sources. Furthermore, the system is compact and can be integrated into existing production lines, minimizing installation and operational costs.
Applications and Industry Impact
Rare earth crystal powder pneumatic conveying systems are widely used in various industrial applications where the handling of fine powders is essential. These systems are commonly employed in rare earth extraction and processing plants, where they are used to transport raw materials, intermediate products, and finished powders between different processing stages. The systems are also used in research and development facilities, where precise material handling is critical for experimental work. By improving the efficiency and safety of material transport, these systems contribute to the overall productivity and sustainability of rare earth processing operations. The ability to handle rare earth powders without compromising their quality makes the system an indispensable tool in the modern rare earth industry.