

[WOKING PRINCIPLE AND FEATURES OF BARLEY MATERIAL PNEUMATIC CONVEYING SYSTEMS]
Shandong HeadPowder Engineering Co., Ltd., commonly known as Headpowder, is a professional manufacturer based in Shandong, China. Specializing in the design, development, and production of pneumatic conveying systems, the company focuses on providing efficient and reliable solutions for handling barley and other bulk materials. With years of industry experience, Headpowder has established itself as a trusted partner in the grain processing sector, delivering high-quality equipment tailored to the specific needs of its clients.

Working Principle of Barley Material Pneumatic Conveying Systems
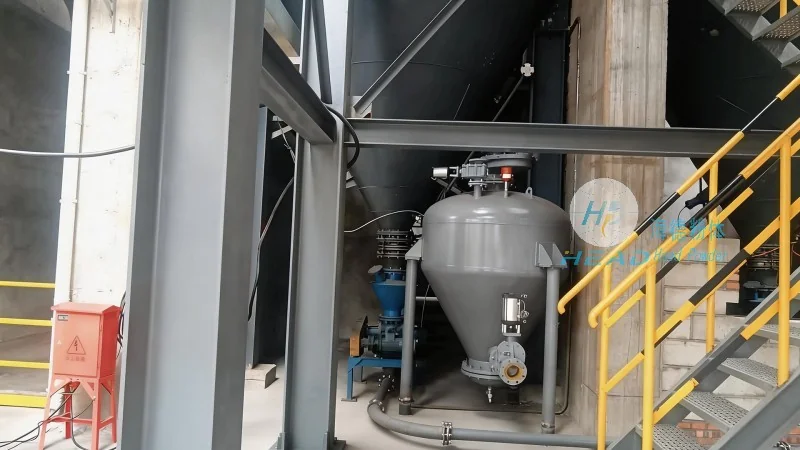
Pneumatic conveying systems operate by transporting bulk materials like barley through a pipeline using a stream of air or gas. The core mechanism involves creating a pressure differential or utilizing vacuum to move the material from the source to the destination. In the case of barley, which is typically a dry, granular product, the system can be configured as either a suction or pressure system. A suction system draws the barley from a hopper or storage silo using a vacuum created by a fan or blower, while a pressure system pushes the material through the pipeline using compressed air. The process ensures that the barley is moved without direct contact with mechanical components, minimizing the risk of contamination and preserving its quality. The system includes key components such as a hopper, a conveyor line, a separator, and a receiver, each playing a crucial role in the efficient transfer of the material.
Key Features and Advantages of Barley Pneumatic Conveying Systems
Headpowder's barley material pneumatic conveying systems offer several distinct advantages that make them ideal for grain processing applications. Firstly, they provide high efficiency in material transfer, capable of moving large volumes of barley over considerable distances with minimal energy consumption. The systems are designed to maintain the integrity of the barley, preventing breakage or damage that could occur with traditional mechanical conveyors. Additionally, pneumatic conveying is highly flexible, allowing for easy integration into existing production lines and the ability to change the direction or destination of the material as needed. Another significant feature is the reduced risk of dust and contamination, as the enclosed pipeline system keeps the barley contained and protected from external elements. This not only improves workplace safety but also maintains the quality of the final product. Furthermore, the systems are easy to clean and maintain, with components that can be disassembled for routine maintenance, ensuring long-term reliability and minimal downtime. The adaptability of these systems to different barley types and processing requirements also enhances their versatility, making them suitable for various industrial applications.
Efficiency and Cost-Effectiveness in Barley Handling
One of the most notable benefits of using pneumatic conveying systems for barley is their superior efficiency compared to traditional methods. The systems can handle large quantities of grain with less labor and lower operational costs. By eliminating the need for manual handling or mechanical equipment that requires frequent maintenance, the overall cost of material transport is significantly reduced. The energy efficiency of these systems is another key factor, as they use less power to move the same amount of barley compared to other conveyance methods. This results in lower electricity bills and a smaller environmental footprint. Additionally, the systems are designed to minimize material loss, ensuring that the maximum amount of barley reaches its intended destination without spillage or waste. This not only saves on material costs but also improves the overall profitability of the grain processing operation.
Environmental and Safety Benefits
Headpowder's barley pneumatic conveying systems are designed with environmental and safety considerations in mind. The enclosed pipeline system effectively reduces dust emissions, which is crucial in grain processing facilities where dust can pose health risks and fire hazards. By containing the barley within the system, the risk of airborne particles is minimized, creating a safer working environment for employees. The systems also help maintain the cleanliness of the processing area, reducing the need for additional cleaning and sanitation measures. Furthermore, the use of compressed air or vacuum in the conveying process eliminates the need for water or other liquids, which can be beneficial in areas with water scarcity or where water usage is restricted. The overall environmental impact of these systems is lower compared to traditional conveyors, making them a more sustainable choice for modern grain processing operations.

Customization and Versatility for Diverse Applications
Headpowder understands that different grain processing facilities have unique requirements, which is why their pneumatic conveying systems are highly customizable. The company offers a range of configurations to suit various barley types, processing capacities, and operational needs. Whether a facility needs a system for short-distance transport or a long-distance pipeline, Headpowder can design a solution that meets the specific demands. The systems can be integrated with existing equipment, such as storage silos, processing units, and packaging lines, ensuring seamless operation. Additionally, the company provides technical support and consultation to help clients select the most appropriate system for their needs, ensuring optimal performance and efficiency. This versatility makes Headpowder's systems suitable for a wide range of applications, from small-scale grain mills to large industrial processing plants.
Conclusion: Reliable Solutions for Barley Processing
Shandong HeadPowder Engineering Co., Ltd. provides advanced pneumatic conveying systems that are designed to meet the demanding needs of barley processing. By combining efficient technology with reliable performance, these systems offer significant advantages in material handling, cost reduction, and environmental safety. With a focus on quality and customer satisfaction, Headpowder continues to be a leader in the grain processing equipment industry, delivering solutions that help clients improve their operations and achieve their business goals. Whether you are a small-scale farmer or a large industrial processor, Headpowder's barley pneumatic conveying systems offer a reliable and effective way to handle your grain with precision and care.