

Working Principle and Features of Long-Distance Material Handling Equipment
Long-distance material handling equipment is a critical component in modern industrial operations, designed to efficiently transport bulk materials over extended distances with precision and reliability. The systems typically operate through a combination of mechanical, electrical, and control mechanisms that work in tandem to ensure smooth and continuous material flow. Understanding the working principle and key features of such equipment is essential for optimizing industrial processes and enhancing operational efficiency.

Company Information
For this discussion, we refer to the expertise and products of Shandong HeadPowder Engineering Co., Ltd., a leading manufacturer based in China. The company specializes in the design, development, and manufacturing of advanced material handling solutions tailored to meet diverse industrial needs. With a strong commitment to quality and innovation, HeadPowder provides reliable equipment that enhances productivity in various sectors, including mining, construction, and logistics.
Working Principle of Long-Distance Material Handling Systems
The core working principle of long-distance material handling equipment revolves around the integration of several key components, including conveyors, drives, control systems, and supporting structures. The system typically begins with the loading of materials at the source point, where they are fed into the conveyor mechanism. The conveyor, often equipped with specialized belts or rollers, transports the materials along the designated path. A powerful drive system, such as electric motors or hydraulic systems, provides the necessary force to move the materials at a controlled speed. The control system, which may include sensors, controllers, and automation software, monitors the operation, adjusts the speed, and ensures the smooth transfer of materials. This integrated approach allows for consistent and efficient material transport over long distances, minimizing downtime and maximizing throughput.
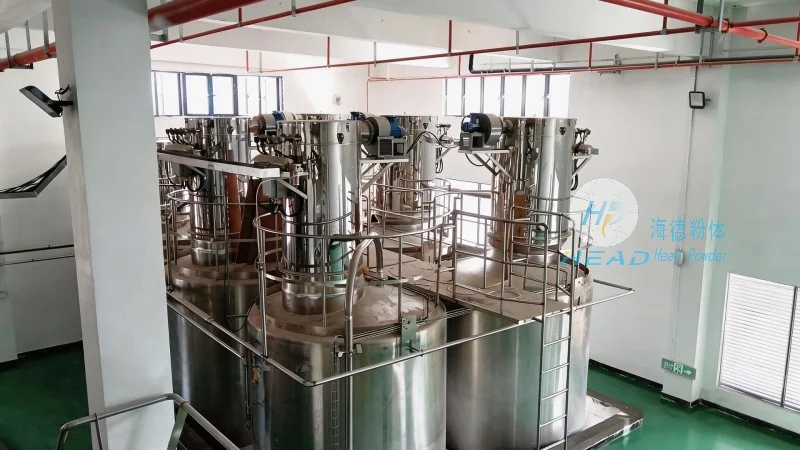
Key Features of Long-Distance Material Handling Equipment
Long-distance material handling equipment from Shandong HeadPowder Engineering Co., Ltd. is characterized by several notable features that enhance its performance and adaptability. One of the primary features is the high efficiency in material transport, achieved through optimized conveyor designs and powerful drive systems. The equipment is engineered to handle a wide range of materials, from granular substances to bulk solids, ensuring versatility in industrial applications. Additionally, the systems are designed with durability and reliability in mind, featuring robust construction and advanced materials that withstand heavy usage and harsh environmental conditions. The control systems are user-friendly and can be integrated with existing industrial automation setups, allowing for seamless operation and easy maintenance. Another key feature is the flexibility in system configuration, as the equipment can be customized to fit specific operational requirements, including different lengths, inclinations, and material handling capacities. This adaptability makes the systems suitable for various industries, from mining operations to construction sites, where efficient material movement is crucial for productivity.
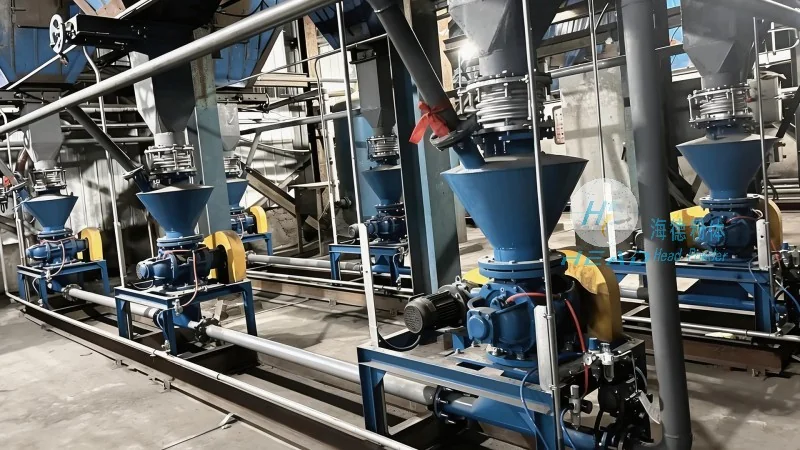
Operational Advantages and Applications
The implementation of long-distance material handling equipment offers significant operational advantages, particularly in terms of productivity and cost-effectiveness. By automating the material transport process, the equipment reduces the need for manual labor, thereby lowering labor costs and minimizing the risk of human error. The consistent and reliable operation of the systems ensures that materials are delivered to their destination on time, improving overall workflow efficiency. Furthermore, the advanced control systems enable real-time monitoring and adjustment, allowing operators to quickly address any issues that may arise during operation. The equipment is widely applied in industries such as mining, where it is used to transport ore from extraction sites to processing facilities; in construction, where it handles building materials like sand, gravel, and cement; and in logistics, where it facilitates the movement of bulk goods in warehouses and distribution centers. In each of these applications, the long-distance material handling equipment from Shandong HeadPowder Engineering Co., Ltd. plays a vital role in optimizing material flow and enhancing operational performance.
Conclusion
In conclusion, long-distance material handling equipment operates on a well-defined principle of integrated mechanical and electrical systems designed to efficiently transport materials over extended distances. The equipment from Shandong HeadPowder Engineering Co., Ltd. stands out for its robust construction, high efficiency, and adaptability, making it a reliable choice for various industrial applications. By understanding the working principle and key features of such equipment, industries can make informed decisions to enhance their operational capabilities and achieve greater productivity. With its commitment to quality and innovation, HeadPowder continues to provide advanced material handling solutions that meet the evolving needs of modern industrial operations.