

What is a Powder Conveyor for Propellants? And What Are Its Design Principles?
Fireworks and military applications rely heavily on the precise handling of propellant powders. A powder conveyor for propellants is a specialized piece of equipment designed to transport these fine, potentially explosive materials safely and efficiently. Understanding its function and the underlying design principles is crucial for anyone involved in the production or handling of such materials.

Powder Conveyors for Propellants: An Overview
At the heart of many industrial processes involving propellant powders is the powder conveyor. These systems are engineered to move materials like black powder, smokeless powder, or other pyrotechnic compounds from one location to another without compromising safety or material integrity. The primary goal is to ensure that the powders are conveyed in a controlled manner, minimizing the risk of dust explosions, caking, or contamination.
HeadPowder, a leading manufacturer based in Shandong, China, specializes in the design and production of such critical equipment. With a strong commitment to safety and performance, the company's products are tailored to meet the stringent requirements of the propellant industry. The company's full name is Shandong HeadPowder Engineering Co., Ltd., and its operations are centered in China, providing a robust foundation for delivering reliable solutions to clients worldwide.
The Design Principles of Propellant Powder Conveyors
The design of a propellant powder conveyor is governed by several key principles aimed at ensuring safety, efficiency, and durability. One of the most critical aspects is the use of explosion-proof components. Since propellant powders are often flammable, the conveyor must be constructed with materials and components that can withstand potential ignition sources, such as static electricity or sparks. This typically involves the use of non-sparking metals, grounding mechanisms, and proper ventilation systems to prevent the accumulation of dust clouds.
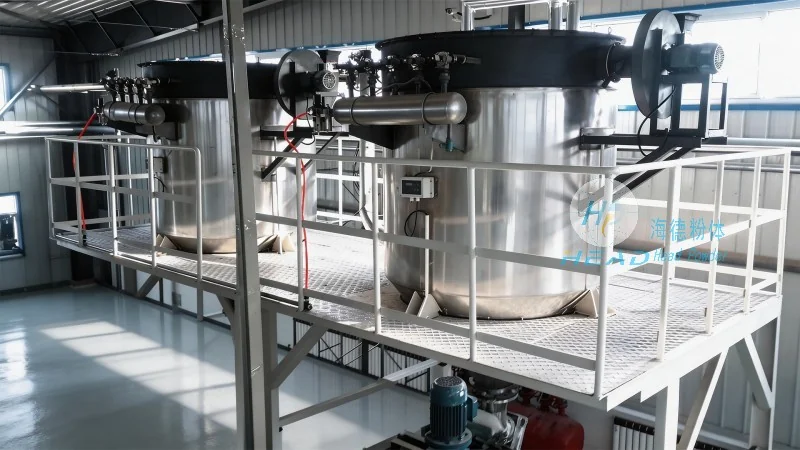
Another essential design consideration is the prevention of material caking and agglomeration. Propellant powders can clump together due to moisture, temperature changes, or handling, which can obstruct the conveyor and reduce its effectiveness. To address this, conveyors often incorporate features like vibration systems, air knives, or rotating paddles that keep the material in a free-flowing state. Additionally, the design may include enclosed or sealed housing to contain dust and prevent environmental contamination.
Efficiency is also a key design goal. Propellant powder conveyors are designed to minimize energy consumption while maximizing material throughput. This is achieved through the use of optimized belt or screw designs, variable speed drives, and efficient drive systems. The goal is to move the required amount of material with the least amount of power, reducing operational costs and environmental impact.
Key Components and Their Functions
Understanding the individual components of a propellant powder conveyor helps in appreciating its overall functionality. The main components typically include a hopper for material storage, a conveyor mechanism (such as a screw or belt), a drive system, and a control panel. The hopper is designed to hold the propellant powder and ensure a consistent feed to the conveyor. The conveyor mechanism then transports the material to the desired location, such as a mixing or loading station.
The drive system, often powered by electric motors, provides the necessary force to move the material along the conveyor. Variable speed drives allow for adjustments based on the material's properties or the required throughput, enhancing flexibility. The control panel enables operators to monitor and adjust the system's parameters, ensuring safe and efficient operation.

Additional components may include dust collection systems, which capture any airborne particles to prevent environmental pollution and maintain a safe working environment. These systems are crucial for compliance with environmental regulations and for protecting the health of workers handling the powders.
Applications and Benefits
Powder conveyors for propellants are used in a variety of applications within the pyrotechnic and military sectors. They are essential in the production of fireworks, where precise dosing of propellant powders is required to achieve the desired effects. In military applications, these conveyors are used to transport propellants for ammunition and explosives, ensuring that the materials are handled safely and efficiently during manufacturing and loading processes.
The benefits of using specialized propellant powder conveyors extend beyond safety and efficiency. By reducing the risk of accidents and improving material handling, these systems enhance overall productivity. They also help in maintaining the quality of the propellant powders, as the controlled environment prevents contamination and degradation. Furthermore, the use of explosion-proof and dust-tight designs ensures compliance with industry standards and regulations, providing peace of mind to manufacturers and users alike.