

What is Sodium Carbonate Material Handling Equipment? What Are Its Design Principles?
Sodium carbonate, commonly known as soda ash, is a widely used chemical in various industrial applications. The efficient and safe transportation of this material is crucial for maintaining production efficiency and ensuring operational safety. This article explores the key aspects of sodium carbonate material handling equipment, focusing on its design principles and the technology behind it.

The Importance of Specialized Equipment for Sodium Carbonate
Due to its chemical properties and the nature of industrial processes, standard material handling systems may not be suitable for sodium carbonate. This chemical is often handled in bulk quantities and requires equipment that can manage its flow characteristics, prevent contamination, and ensure compliance with safety regulations. Specialized equipment is therefore essential to optimize the handling of sodium carbonate, reducing operational risks and enhancing overall productivity.
Design Principles of Sodium Carbonate Material Handling Equipment
The design of sodium carbonate material handling equipment is guided by several critical principles that address the unique challenges of handling this chemical. These principles include material compatibility, flow control, safety features, and energy efficiency. Each component of the system is carefully engineered to meet these standards, ensuring reliable performance in industrial settings.

Key Components and Technologies
Modern sodium carbonate material handling equipment typically incorporates several key components and technologies. These may include conveyor systems, storage silos, feeding mechanisms, and control systems. For example, belt conveyors are commonly used for transporting bulk sodium carbonate due to their ability to handle large volumes and maintain consistent flow rates. Storage silos are designed with materials that are resistant to the chemical's corrosive properties, ensuring long-term durability and safety.
Material Compatibility and Safety Considerations
One of the most important design considerations is material compatibility. The equipment must be constructed from materials that are resistant to sodium carbonate's chemical effects, such as corrosion or degradation. Common materials used include stainless steel, special alloys, and coated components. Additionally, safety features are integrated into the design to protect operators and prevent accidents. These may include explosion-proof designs, emergency stop mechanisms, and monitoring systems that alert operators to any deviations from normal operating conditions.
Energy Efficiency and Operational Performance
Efficient energy use is a key design principle for modern material handling equipment. By optimizing the design of components like conveyors and motors, manufacturers can reduce energy consumption while maintaining or improving performance. This not only lowers operational costs but also aligns with sustainability goals in industrial operations. Advanced control systems and variable speed drives are often employed to adjust the equipment's operation based on the actual demand, further enhancing energy efficiency.
Application in Industrial Processes
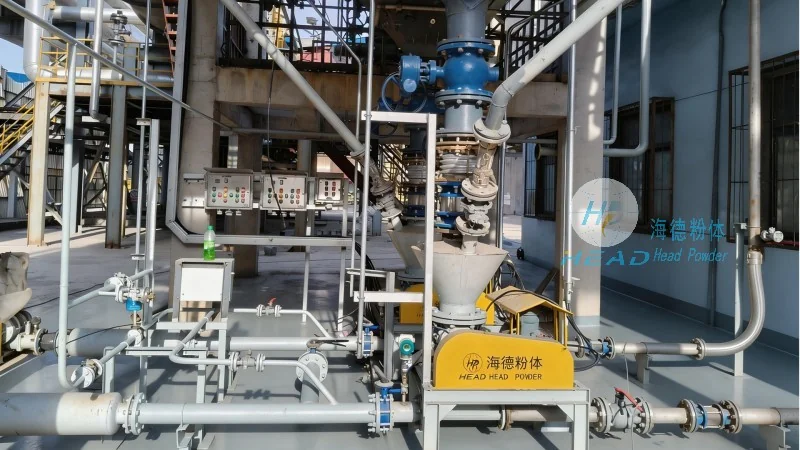
Sodium carbonate material handling equipment is widely used in various industrial sectors, including chemical manufacturing, glass production, and water treatment. In these applications, the equipment plays a critical role in ensuring the smooth flow of materials and supporting the overall production process. The design principles discussed above are tailored to meet the specific requirements of each industry, providing customized solutions that enhance operational efficiency and safety.
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of specialized material handling equipment for industrial chemicals. With a focus on innovation and quality, HeadPowder provides tailored solutions for handling sodium carbonate and other chemicals. The company's expertise in material science and engineering ensures that its products meet the highest standards of performance, safety, and durability. HeadPowder's commitment to customer satisfaction and technological advancement has made it a trusted partner in the chemical processing industry.