

Pneumatic Conveying of Bentonite Powder: A Solution for Overcoming Distance Limitations in Material Handling
For industries dealing with bulk materials like bentonite powder, efficient and reliable material handling is crucial. Traditional methods often face challenges when it comes to transporting these powders over long distances or across complex layouts. This is where pneumatic conveying technology steps in, offering a versatile solution that can overcome distance limitations and streamline operations. In this context, we explore the capabilities of pneumatic conveying systems tailored for bentonite powder, highlighting how they enhance productivity and operational efficiency.

Understanding Pneumatic Conveying Technology
Pneumatic conveying uses air or gas to transport solid materials through a pipeline system. Unlike mechanical conveying methods, which rely on belts, buckets, or screws, pneumatic systems utilize pressure differentials to move powders. This approach is particularly effective for fine powders such as bentonite, which can be prone to caking or segregation under traditional handling conditions. The technology operates by creating a flow of air that draws or pushes the powder through the pipeline, ensuring consistent and controlled movement. There are two primary types of pneumatic conveying: pressure and vacuum systems. Pressure systems use compressed air to push the material, while vacuum systems use a vacuum to pull it. Both methods can be adapted to suit specific operational needs, including varying distances and material characteristics.
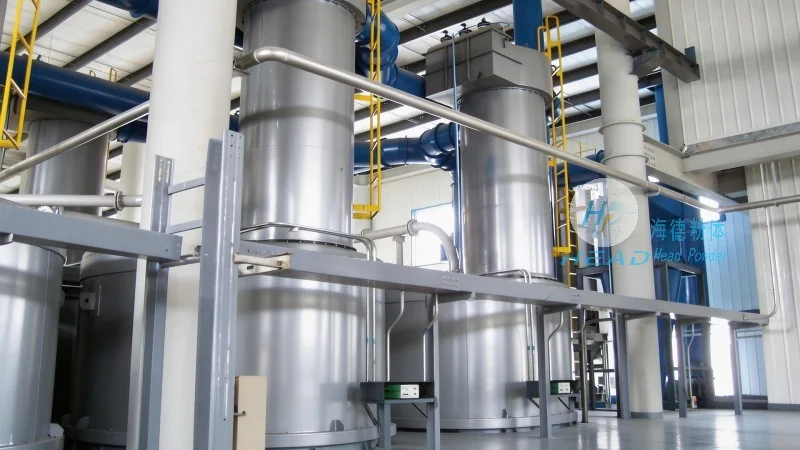
Benefits of Pneumatic Conveying for Bentonite Powder
Implementing pneumatic conveying for bentonite powder offers several key advantages. First, it significantly reduces the risk of material degradation or contamination. Unlike manual handling or mechanical systems that may cause dust or particle breakdown, pneumatic systems maintain the integrity of the powder. This is critical for applications where the quality of bentonite powder directly impacts downstream processes, such as in the paper, foundry, or chemical industries. Second, pneumatic conveying enhances safety by minimizing exposure to dust and reducing the need for manual handling. This not only improves workplace safety but also aligns with regulatory requirements for dust control. Third, the technology improves operational efficiency by allowing for continuous, automated material transport. This eliminates bottlenecks associated with traditional methods and enables real-time monitoring and control of the conveying process. Additionally, pneumatic systems can be integrated with other processing equipment, creating a seamless material flow from storage to processing. This integration further optimizes production cycles and reduces downtime.

Overcoming Distance Limitations with Advanced Systems
One of the most significant challenges in material handling is the need to transport materials over long distances without compromising efficiency or quality. Traditional conveying methods may struggle with distances exceeding a few hundred meters, as they often require multiple transfer points or complex infrastructure. Pneumatic conveying, however, can effectively transport bentonite powder over much greater distances, often up to several kilometers, depending on the system design and operational parameters. This capability is achieved through the use of high-pressure air or vacuum systems that maintain consistent flow rates and pressure differentials throughout the pipeline. Advanced control systems, such as variable frequency drives (VFDs) and pressure sensors, ensure that the conveying process remains stable even over long distances. These systems can also adapt to changes in material density or flow characteristics, ensuring consistent performance. For example, in industrial settings where bentonite is used in large-scale production, pneumatic conveying allows for centralized storage and distribution of the powder to multiple processing units, eliminating the need for separate storage at each location. This not only reduces storage costs but also improves material traceability and quality control.
Customized Solutions from Shandong HeadPowder Engineering Co., Ltd.
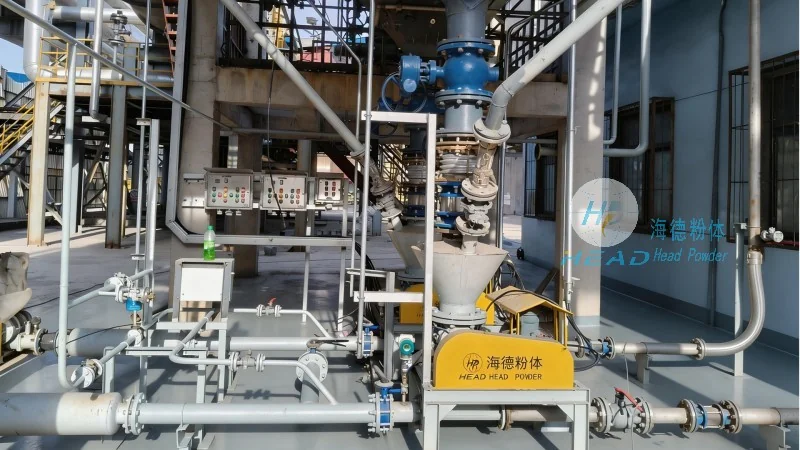
Shandong HeadPowder Engineering Co., Ltd., a leading provider of material handling solutions, specializes in designing and manufacturing pneumatic conveying systems tailored to the unique needs of bentonite powder applications. With years of experience in the industry, the company understands the specific challenges associated with handling fine powders and has developed innovative solutions to address them. The company’s team of engineers works closely with clients to assess their operational requirements, including distance, flow rates, and material characteristics, to design a customized system that meets their specific needs. Whether it’s a pressure or vacuum system, the company offers a range of options to suit different operational scenarios. The systems are built with high-quality materials, such as stainless steel and corrosion-resistant components, ensuring durability and long-term performance. Additionally, the company provides comprehensive after-sales support, including maintenance services and technical assistance, to ensure that the systems operate at optimal efficiency. By partnering with Shandong HeadPowder Engineering Co., Ltd., clients can benefit from a reliable and efficient material handling solution that enhances their productivity and reduces operational costs.
Conclusion: Enhancing Material Handling with Pneumatic Conveying
In conclusion, pneumatic conveying represents a highly effective solution for transporting bentonite powder over long distances while maintaining quality and efficiency. The technology offers numerous benefits, including improved safety, reduced material degradation, and enhanced operational efficiency. With the right system design and implementation, industries can overcome the limitations of traditional material handling methods and achieve seamless material flow. Shandong HeadPowder Engineering Co., Ltd. stands as a trusted partner in providing customized pneumatic conveying solutions that meet the specific needs of bentonite powder applications. By leveraging advanced technology and expert engineering, the company helps clients optimize their material handling processes, leading to increased productivity and cost savings. As industries continue to seek more efficient and sustainable solutions, pneumatic conveying remains a key technology for handling bulk materials like bentonite powder, ensuring that operations run smoothly and reliably.