

Principle and Working Scene Characteristics of Corn Cob Material Pneumatic Conveying Equipment
For industries dealing with corn cob material, efficient and reliable material handling is crucial. Pneumatic conveying equipment has emerged as a key solution, offering a seamless way to transport corn cob from storage to processing units. This article explores the underlying principles of such equipment and highlights the specific characteristics of its application in various working scenes.
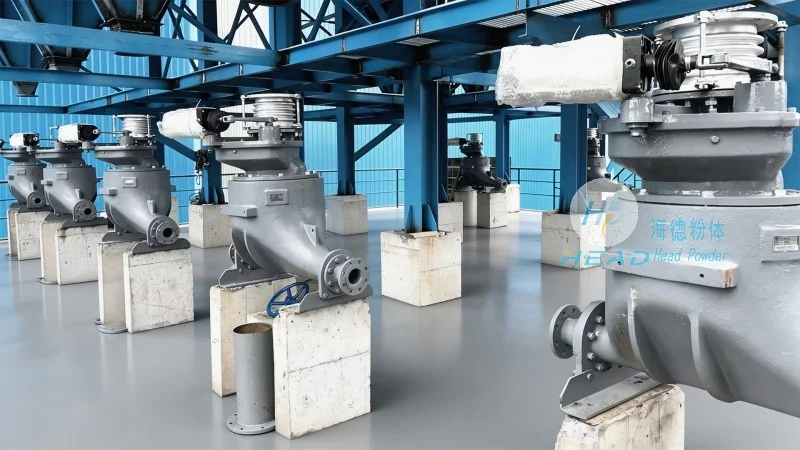
Understanding the Core Principle of Pneumatic Conveying for Corn Cob Material
Pneumatic conveying systems operate by using air to move bulk materials like corn cob through a pipeline network. The fundamental principle involves creating a pressure differential or utilizing vacuum to draw or push the material along. In the case of corn cob, which is a light, dry, and somewhat abrasive material, the choice of conveying method—whether it's a negative pressure (suction) system or a positive pressure (blowing) system—plays a critical role in ensuring efficient transport with minimal wear and tear on the equipment.
The system typically consists of a hopper, a conveyor line, and a control unit. The corn cob is fed into the hopper, where it is then drawn into the pipeline by a vacuum created by a fan or blower. The air and material mixture travels through the pipeline to the destination point, such as a storage silo or a processing machine. The separation of air and material at the receiving end is achieved through a cyclone separator or a filter, ensuring that the corn cob is delivered without contamination from the conveying air.

Key Working Scene Characteristics of Corn Cob Pneumatic Conveying Equipment
The application of corn cob pneumatic conveying equipment varies across different industrial sectors, each with unique requirements that the equipment must address. In the feed and animal nutrition industry, for instance, the equipment is used to transport corn cob from storage to feed mills, where it is processed into animal feed. The key characteristics here include high capacity, as large volumes of corn cob need to be moved quickly, and the ability to handle the material's light and dusty nature without causing blockages or excessive wear.
In the biomass energy sector, corn cob is often used as a fuel source for power generation. The pneumatic conveying system is essential for transporting the material from the field or storage to the boiler or gasifier. The working scene characteristics in this context emphasize the need for durability and resistance to abrasion, as the corn cob can be hard and abrasive. Additionally, the system must be capable of operating continuously over long periods, ensuring a steady supply of fuel to the energy production units.

Another important application is in the manufacturing of bio-based products, where corn cob is used as a raw material for various industrial processes. The equipment must be able to handle the material's irregular shape and varying moisture content, which can affect its flow characteristics. The working scene characteristics in this case include the need for precise control over the material flow rate and the ability to integrate seamlessly with other processing equipment, such as grinders or mixers.

About Shandong HeadPowder Engineering Co., Ltd.
HeadPowder, or Shandong HeadPowder Engineering Co., Ltd., is a leading manufacturer of pneumatic conveying equipment tailored for corn cob and other bulk materials. Based in Shandong, China, the company specializes in designing and producing customized solutions that meet the specific needs of its clients. With years of experience in the industry, HeadPowder has developed a reputation for delivering high-quality, efficient, and reliable equipment that enhances productivity and reduces operational costs for its customers.
The company's products are engineered to handle the unique challenges posed by corn cob material, such as its light weight, abrasive nature, and potential for dust generation. By leveraging advanced technology and rigorous quality control, HeadPowder ensures that its pneumatic conveying systems operate at peak efficiency, minimizing downtime and maximizing material throughput. Whether for feed processing, biomass energy, or bio-product manufacturing, HeadPowder's equipment is designed to meet the demands of modern industrial applications.