

Principle and Working Scene Characteristics of Intelligent Bulk Bag Unloading Pneumatic Conveying Eq
Intelligent bulk bag unloading pneumatic conveying equipment represents a sophisticated solution for the efficient and safe transfer of bulk materials from large flexible containers, commonly referred to as super sacks or bulk bags. This technology has become increasingly vital in modern industrial settings, where the handling of fine powders and granules demands precision, reliability, and automation. The equipment integrates advanced control systems, sensors, and mechanical components to streamline the material handling process, reducing manual labor, minimizing material loss, and enhancing overall operational efficiency. By leveraging pneumatic conveying principles, the system ensures that bulk materials are transferred from the bag to the processing or storage system with minimal disruption and maximum safety, making it an essential asset in sectors such as chemical, food, pharmaceutical, and mining.

Core Principles of the Equipment
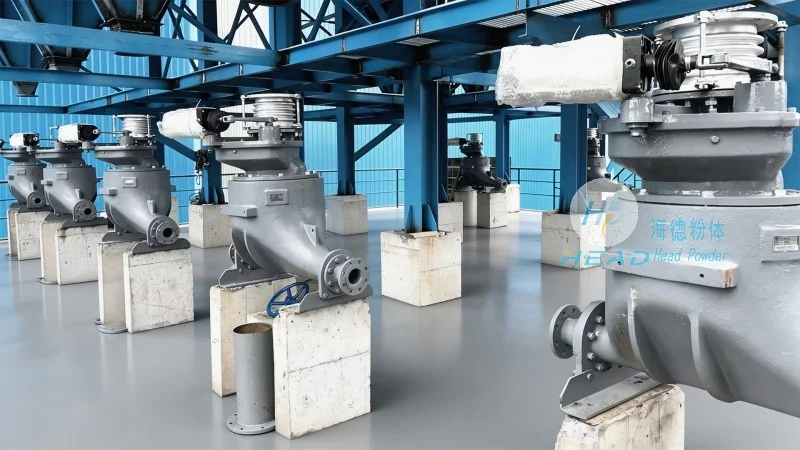
The operational principle of intelligent bulk bag unloading pneumatic conveying equipment is centered on the use of compressed air to create a pressure differential that draws the material from the bulk bag into the conveying line. The process typically begins with the placement of the bulk bag onto a discharger unit, which is equipped with a valve mechanism to control the flow of air and material. As air is introduced into the bag, it creates a vacuum in the conveying line, causing the material to be drawn out and transported through the pipeline. Key components of the system include the bulk bag discharger, airlock valve, and pneumatic conveying line, each playing a critical role in ensuring a smooth and continuous flow. The intelligent features of the equipment often involve real-time monitoring of parameters such as pressure, flow rate, and bag weight, allowing for automated adjustments to maintain optimal performance. This automation not only reduces the risk of operational errors but also enhances the system's adaptability to varying material characteristics and processing requirements.
Working Scene Characteristics
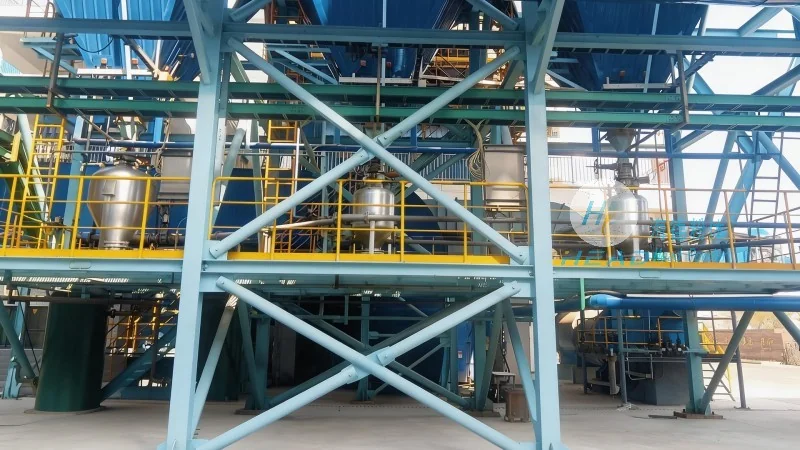
The working scene characteristics of intelligent bulk bag unloading pneumatic conveying equipment are designed to accommodate diverse industrial environments and application needs. These systems are engineered for both indoor and outdoor use, with robust construction that can withstand harsh conditions like dust, moisture, and temperature fluctuations. The equipment is particularly well-suited for high-volume material handling operations, where the rapid and efficient transfer of large quantities of bulk materials is essential. For instance, in chemical manufacturing plants, the system can handle hazardous powders with strict safety protocols, ensuring that the material is transferred without exposing personnel to dangerous substances. In food processing facilities, the equipment is often equipped with sanitary designs to comply with food safety regulations, allowing for the handling of sensitive ingredients like flour, sugar, or spices. The adaptability of the system also makes it ideal for research and development laboratories, where different materials may need to be processed on an as-needed basis, providing flexibility and precision in material handling. Additionally, the system's ability to integrate with existing production lines enhances its utility, making it a cost-effective solution for upgrading or expanding material handling capabilities.

Company Profile: HeadPowder
HeadPowder, formally known as Shandong HeadPowder Engineering Co., Ltd., is a prominent manufacturer specializing in the design, development, and supply of advanced material handling equipment. Headquartered in Shandong, China, the company has established itself as a leader in the industry, delivering high-quality, reliable solutions tailored to the specific needs of various sectors. HeadPowder's commitment to innovation and customer-centric approaches is reflected in their comprehensive product line, which includes intelligent bulk bag unloading systems, pneumatic conveying equipment, and other specialized material handling solutions. The company's engineering expertise and rigorous quality control processes ensure that each product meets or exceeds industry standards, providing customers with durable and efficient equipment that enhances operational efficiency and safety. With a strong focus on research and development, HeadPowder continuously improves its technologies to meet evolving industry demands, offering customized solutions that address unique challenges faced by clients. The company's reputation for excellence and reliability has earned it a loyal customer base, making it a trusted partner for businesses seeking advanced material handling solutions.