

Bentonite Pneumatic Conveying Solutions
Introduction to Bentonite Pneumatic Conveying Systems

Bentonite, a versatile clay material widely used in various industrial processes, requires efficient and reliable transport methods to ensure smooth operations. Pneumatic conveying systems offer an effective solution for handling bentonite, combining precision, safety, and adaptability. This article explores the benefits and applications of bentonite pneumatic conveying solutions, highlighting how they enhance material handling efficiency in industrial settings.
HeadPowder: Your Trusted Partner in Material Handling
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading provider of specialized material handling equipment and solutions. With a strong commitment to innovation and quality, HeadPowder has established itself as a trusted partner for industries relying on efficient transport of bulk materials like bentonite. HeadPowder's expertise in pneumatic conveying technology ensures that clients receive tailored solutions that meet their specific operational needs.
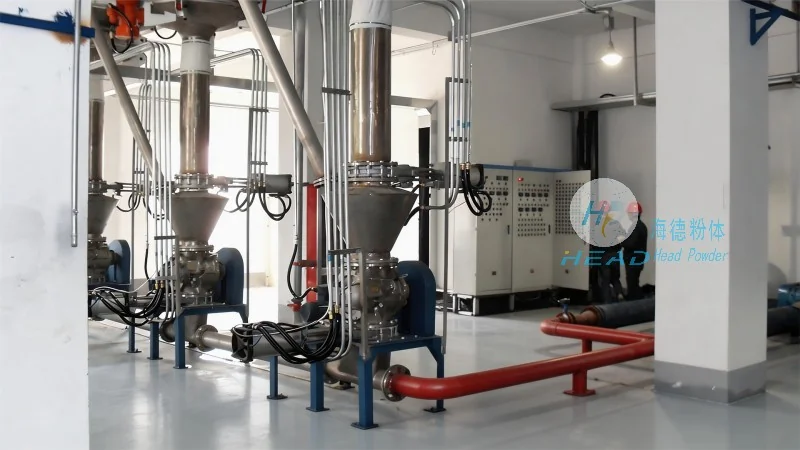
Key Features of Our Bentonite Pneumatic Conveying Solutions
HeadPowder's bentonite pneumatic conveying systems are designed with several key features that enhance performance and reliability. These systems utilize air pressure to move bentonite from one location to another, eliminating the need for mechanical components that may cause wear and tear. The technology ensures minimal product degradation, maintaining the quality of bentonite during transport. Additionally, the systems are equipped with advanced control mechanisms that allow for precise flow regulation, optimizing material movement based on operational requirements.
Application Scenarios and Operational Benefits
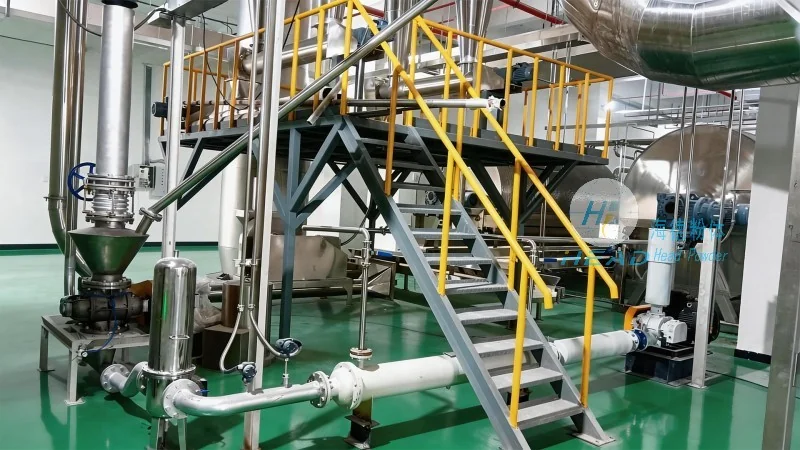
Bentonite pneumatic conveying solutions find applications in multiple industries, including pharmaceuticals, food processing, and chemical manufacturing. In pharmaceutical production, for instance, the systems ensure hygienic and dust-free transport of bentonite, adhering to stringent quality standards. The operational benefits include reduced labor costs, as automated systems minimize manual handling, and improved safety by eliminating exposure to dust and other hazards. Furthermore, the systems enhance production throughput by enabling continuous material flow, which is crucial for maintaining high output levels.
Technical Advantages and Efficiency Enhancements

The technical design of HeadPowder's bentonite pneumatic conveying systems incorporates several advantages that boost efficiency. The use of positive pressure or negative pressure systems allows for flexible configuration based on the distance and layout of the transport route. The systems are equipped with high-efficiency filters that prevent dust accumulation and maintain air quality, ensuring compliance with environmental regulations. Additionally, the integration of sensors and monitoring systems provides real-time data on system performance, enabling proactive maintenance and reducing downtime.
Customization and Compliance with Industry Standards
HeadPowder understands that each industrial application has unique requirements. Therefore, the company offers customized bentonite pneumatic conveying solutions tailored to specific client needs. Whether it's a small-scale operation or a large industrial facility, HeadPowder's engineers work closely with clients to design systems that optimize material flow and operational efficiency. The company adheres to international standards such as ISO and CE, ensuring that all products meet the highest quality and safety benchmarks. This commitment to compliance provides clients with peace of mind regarding the reliability and performance of the conveying systems.