

How to Choose the Right Pneumatic Conveying System for Your Rare Earth Powder Handling Process?
When it comes to managing rare earth powder handling processes, selecting the appropriate pneumatic conveying system is a critical decision that impacts operational efficiency, product integrity, and overall process reliability. The right system ensures that your rare earth powders are transported safely, efficiently, and with minimal degradation, which is essential for maintaining the quality and value of these valuable materials. This guide will help you understand the key factors to consider when choosing a pneumatic conveying system tailored to your specific rare earth powder handling needs.

Understanding the Importance of Pneumatic Conveying for Rare Earth Powders
Rare earth powders, such as neodymium, praseodymium, and cerium compounds, are characterized by their fine particle size, high reactivity, and potential for dust generation. Traditional bulk material handling methods may not be suitable due to the risk of particle degradation, contamination, or equipment wear. Pneumatic conveying systems offer a solution by using air or other gases to transport powders through pipelines, providing a closed-loop system that minimizes exposure to the environment and reduces the risk of product loss or contamination. This method is particularly advantageous for rare earth powders, which require precise control over particle flow and moisture content to preserve their chemical properties and market value.
Key Factors to Consider When Selecting a Pneumatic Conveying System
Choosing the right pneumatic conveying system for your rare earth powder handling process involves evaluating several key factors to ensure optimal performance and compatibility with your specific application. The first consideration is the material characteristics of the rare earth powder, including particle size distribution, bulk density, and flowability. These properties determine the appropriate conveying velocity, pressure, and system design to prevent blockages or excessive wear on components. Additionally, the system must be capable of handling the specific chemical and physical properties of the rare earth powders, such as their reactivity with air or moisture, to maintain product integrity throughout the conveying process.

Another critical factor is the system's ability to handle variations in material feed, including batch sizes and feed rates. A well-designed pneumatic conveying system should be flexible enough to accommodate changes in production volume without compromising efficiency or product quality. This flexibility is essential for rare earth powder handling, where production schedules may vary based on market demand or processing requirements. Furthermore, the system must be equipped with features that ensure safety and compliance with industry standards, such as dust suppression mechanisms, explosion-proof designs, and proper ventilation to protect both personnel and the environment.
HeadPowder: Your Partner in Rare Earth Powder Handling Solutions
At Shandong HeadPowder Engineering Co., Ltd., we specialize in providing customized pneumatic conveying systems tailored to the unique needs of rare earth powder handling processes. With our headquarters in Shandong, China, our team of experts has extensive experience in designing and implementing efficient, reliable, and cost-effective solutions for a wide range of rare earth powder applications. Our commitment to quality and innovation ensures that our systems meet the highest standards of performance and durability, providing long-term value to our clients.

Our pneumatic conveying systems are engineered to handle the specific challenges associated with rare earth powders, including their fine particle size, high reactivity, and potential for dust generation. We offer a range of system configurations, from low-pressure dilute phase systems to high-pressure dense phase systems, to suit different production requirements and material characteristics. Each system is designed with precision to ensure optimal conveying efficiency, minimal product degradation, and maximum safety for both the material and personnel.
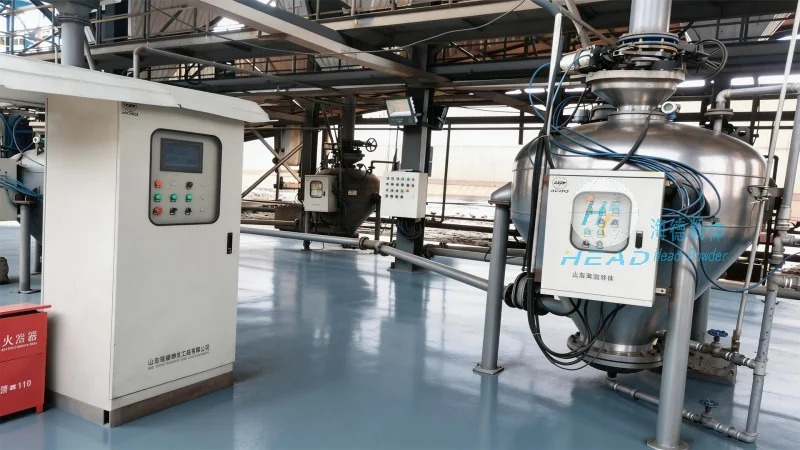
Our team works closely with clients to understand their specific rare earth powder handling challenges and develop customized solutions that address their unique needs. Whether you need a system for material transfer between processing stages, storage and retrieval, or integration with existing production lines, we provide comprehensive support from initial design and engineering to installation and maintenance. By choosing HeadPowder, you can trust that your rare earth powder handling process will be optimized for efficiency, reliability, and product quality.
Conclusion: Making the Right Choice for Your Rare Earth Powder Handling Process
Selecting the right pneumatic conveying system for your rare earth powder handling process is a decision that requires careful consideration of material properties, operational requirements, and safety standards. By partnering with a reputable company like Shandong HeadPowder Engineering Co., Ltd., you can ensure that your system is tailored to your specific needs, providing long-term benefits in terms of efficiency, product quality, and operational reliability. With our expertise and commitment to excellence, we are dedicated to helping you achieve the best possible results in your rare earth powder handling operations.