

Working Principle and Features of Powdered Seasoning Pneumatic Conveying System Equipment
For industries dealing with powdered seasonings, efficient and reliable material handling is crucial. The powdered seasoning pneumatic conveying system equipment, offered by Shandong HeadPowder Engineering Co., Ltd., is a specialized solution designed to address the unique challenges of transporting fine powders like spices, seasonings, and other similar products. This article will explore the working principle and key features of such systems, highlighting how they enhance operational efficiency and product integrity.

Understanding the Working Principle of Powdered Seasoning Pneumatic Conveying Systems
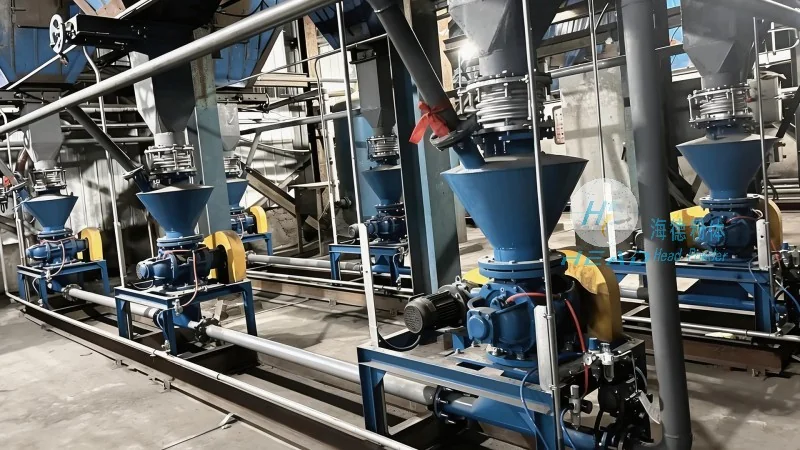
The core of a powdered seasoning pneumatic conveying system lies in its ability to transport dry powders through a pressurized or vacuum environment using air or gas as the conveying medium. The system typically operates on one of two fundamental principles: pressure or vacuum. In a pressure system, air is forced into a hopper containing the powder, creating a positive pressure that pushes the material through a pipeline to the destination. Conversely, a vacuum system uses a suction mechanism to draw the powder from the source into the conveying line. Both methods rely on the principle of fluidization, where the powder particles are suspended and transported by the moving air stream. The system components include a hopper for material storage, a feeder to control the flow rate, a conveying line (often with bends and filters), and a receiver for the discharged material. The air flow is managed by a blower or vacuum pump, ensuring consistent pressure or vacuum levels throughout the system. This mechanism allows for continuous, dust-free, and hygienic transport of powdered seasonings, minimizing product degradation and contamination risks.

Key Features of Powdered Seasoning Pneumatic Conveying Equipment
Shandong HeadPowder Engineering Co., Ltd. specializes in designing and manufacturing pneumatic conveying systems tailored to the demands of the seasoning industry. The equipment features several notable characteristics that enhance performance and user experience. Firstly, the system is designed for high efficiency in material transport, with minimal pressure drop and consistent flow rates, ensuring reliable delivery of powdered seasonings to processing or packaging areas. Secondly, it offers excellent dust control, as the enclosed system prevents airborne particles from contaminating the environment or product. This is particularly important for food-grade applications, where hygiene and product purity are paramount. Thirdly, the equipment is built for durability and easy maintenance, with components such as wear-resistant hoppers and filters that reduce the need for frequent repairs. The modular design allows for easy integration into existing production lines, and the system can be customized to handle various powder types and flow rates. Additionally, the use of advanced control systems enables precise regulation of air pressure and flow, optimizing energy consumption and operational costs. These features collectively make the pneumatic conveying system an ideal choice for businesses seeking to streamline their seasoning handling processes while maintaining product quality and safety standards.
Benefits of Implementing Powdered Seasoning Pneumatic Conveying Systems
Adopting a pneumatic conveying system for powdered seasonings brings numerous benefits to manufacturers. The primary advantage is the significant improvement in operational efficiency, as the system allows for continuous, unattended operation, reducing labor costs and increasing production throughput. The dust-free environment also contributes to a safer workplace, minimizing the risk of respiratory issues among employees handling fine powders. Furthermore, the enclosed system prevents product cross-contamination, which is critical in food processing industries where maintaining product integrity is essential. The system’s ability to handle a wide range of powder types, from fine spices to coarse seasonings, makes it versatile and adaptable to different production needs. Another key benefit is the reduction in product loss and degradation, as the system minimizes exposure to air and moisture, which can affect the flavor and shelf life of seasonings. Finally, the energy efficiency of modern pneumatic conveying systems, combined with lower maintenance requirements, results in long-term cost savings for businesses. Overall, the implementation of such systems enhances both productivity and product quality, making them a valuable investment for seasoning manufacturers.