

Working Principle and Features of Activated Carbon Pneumatic Conveying Equipment
Activated carbon is a critical material in various industrial applications, including air purification, water treatment, and chemical processing. The efficient and reliable transportation of activated carbon from storage to processing units is essential for maintaining operational efficiency and product quality. Pneumatic conveying systems have emerged as a preferred method for handling activated carbon due to their ability to transport powders and granules in a controlled manner. This article explores the working principle and key features of activated carbon pneumatic conveying equipment, highlighting how these systems enhance industrial processes.

Working Principle of Activated Carbon Pneumatic Conveying Equipment
The core of an activated carbon pneumatic conveying system lies in its ability to use air or gas to transport solid materials. The process typically involves several key components and steps. First, the activated carbon is loaded into a hopper or storage silo. From there, the material is drawn into a conveying line by a vacuum or pressure source. The system uses either a vacuum (negative pressure) or pressure (positive pressure) method to move the carbon. In a vacuum system, a fan or vacuum pump creates a low-pressure environment that pulls the carbon particles through the pipeline. In a pressure system, compressed air pushes the material forward. The conveying line may include bends, filters, and cyclones to ensure smooth flow and prevent blockages. The system also incorporates control valves and sensors to regulate the flow rate and maintain consistent pressure, ensuring the activated carbon reaches its destination without degradation or loss.

Key Features of Activated Carbon Pneumatic Conveying Equipment
Activated carbon pneumatic conveying equipment from Shandong HeadPowder Engineering Co., Ltd. offers several advantages that make it ideal for industrial applications. One of the primary features is its high efficiency in material handling. The system can transport activated carbon over long distances with minimal loss, ensuring that the material remains intact and free from contamination. This efficiency is crucial for maintaining the quality of the activated carbon, which is often used in sensitive applications like air filtration and water purification. Another key feature is the system's ability to handle a wide range of particle sizes and moisture contents. Whether the activated carbon is in the form of fine powders or larger granules, the equipment can adapt to different material characteristics, making it versatile for various industrial needs. Additionally, the equipment is designed with durability and low maintenance in mind. High-quality materials and robust construction ensure that the system operates reliably over extended periods, reducing downtime and maintenance costs. The system also incorporates advanced control systems that allow for precise regulation of flow rates and pressure, enhancing operational control and safety. Environmental considerations are also a significant feature, as the equipment is designed to minimize dust emissions and ensure compliance with environmental regulations. This makes it an environmentally friendly solution for transporting activated carbon, aligning with modern industrial sustainability goals.
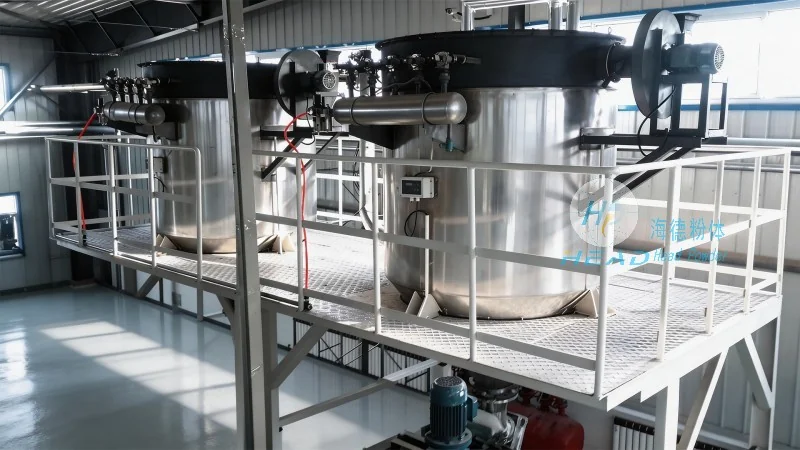
About Shandong HeadPowder Engineering Co., Ltd.
Shandong HeadPowder Engineering Co., Ltd., commonly known as HeadPowder, is a leading manufacturer of industrial conveying equipment, including activated carbon pneumatic conveying systems. With its headquarters located in Shandong, China, the company has established itself as a trusted provider of high-quality solutions for material handling in various industries. HeadPowder specializes in designing and manufacturing equipment that meets the specific needs of its clients, ensuring that each system is tailored to the unique requirements of the application. The company's commitment to quality and innovation has enabled it to deliver reliable and efficient solutions that enhance operational performance and reduce costs for its customers. By leveraging advanced technology and rigorous quality control processes, HeadPowder ensures that its products meet the highest standards in the industry, providing long-term value and satisfaction to its clients.