

What is a Small Gravel Material Handling System Equipment? And What Are Its Design Principles?
Small gravel material handling systems are vital components in numerous industrial and construction operations, engineered to efficiently transport and manage loose gravel and similar bulk materials. These systems play a crucial role in maintaining operational efficiency and safety in environments where handling such materials is commonplace. The equipment used within these systems is specifically designed to accommodate the unique characteristics of small gravel, including its size, weight, and flow properties, ensuring optimal performance under various conditions.

Key Components of Small Gravel Material Handling Equipment
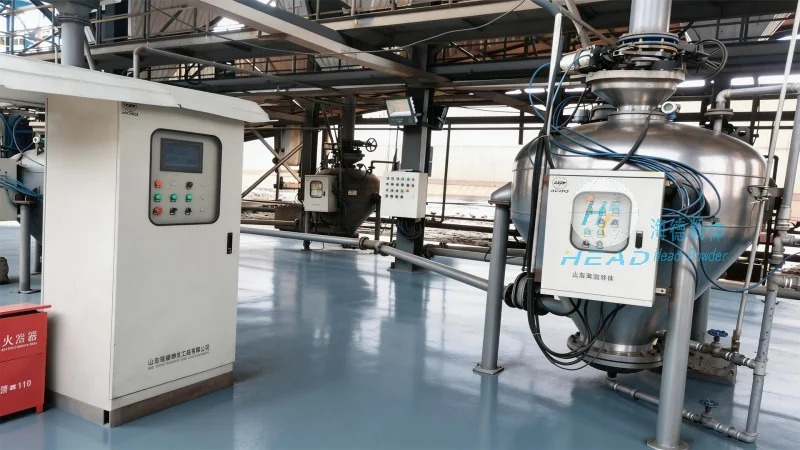
HeadPowder, a prominent manufacturer headquartered in Shandong, China, specializes in providing advanced equipment for small gravel material handling. The fundamental components of these systems typically consist of feeders, conveyors, and control mechanisms. Feeders are responsible for uniformly distributing the gravel into the conveyor system, guaranteeing consistent material flow. Conveyors, such as belt or screw types, transport the material through the system, while control mechanisms manage the speed and direction of movement. Each component is meticulously engineered to work in harmony, optimizing the overall material handling performance and minimizing operational disruptions.

Design Principles for Efficient Material Handling
The design principles of small gravel material handling systems prioritize efficiency, reliability, and safety. Engineers at Shandong HeadPowder Engineering Co., Ltd. conduct thorough analyses of material characteristics, system capacity, and operational environments to develop tailored solutions. For example, the selection of conveyor type depends on factors like gravel size and required throughput. Belt conveyors are often favored for high-volume applications due to their high capacity and durability, whereas screw conveyors are suitable for more compact or vertical transport needs. Integrated control systems provide real-time monitoring and adjustment capabilities, enabling operators to maintain optimal performance and respond to changes in material flow or system conditions.

Applications and Benefits in Industrial Settings
Small gravel material handling systems find extensive applications across industries including mining, construction, and recycling. In mining operations, these systems efficiently transport extracted gravel from processing sites to storage or further processing areas, streamlining the workflow and reducing manual handling efforts. In construction, they assist in moving gravel for road building, landscaping, and foundation work, contributing to project timelines and quality. The benefits of utilizing specialized equipment from HeadPowder include enhanced productivity, reduced labor costs, and improved workplace safety. By automating the material handling process, these systems minimize risks associated with manual handling and ensure consistent material flow, leading to better project outcomes and operational success.
Customization and Maintenance Considerations
HeadPowder recognizes that each industrial application has distinct requirements, which is why they offer customized solutions for small gravel material handling. Customers can specify system capacity, conveyor length, and additional features such as dust control or material sorting to align with their specific operational needs. Regular maintenance is essential to ensure the longevity and efficiency of the equipment. Shandong HeadPowder Engineering Co., Ltd. provides comprehensive maintenance services and spare parts support to their clients, ensuring that the systems operate at peak performance. Proper maintenance practices include regular inspections of conveyor belts, motor checks, and cleaning of components to prevent wear and tear, thereby extending the equipment's service life and maintaining optimal operational efficiency.