

Working Principle and Features of Nitrile Rubber Pneumatic Conveying System Equipment
Shandong HeadPowder Engineering Co., Ltd. specializes in providing advanced solutions for material handling, with a focus on nitrile rubber pneumatic conveying systems. These systems are designed to efficiently transport nitrile rubber and related materials through an air-driven process, offering significant advantages in industrial applications.

Working Principle of Nitrile Rubber Pneumatic Conveying Systems
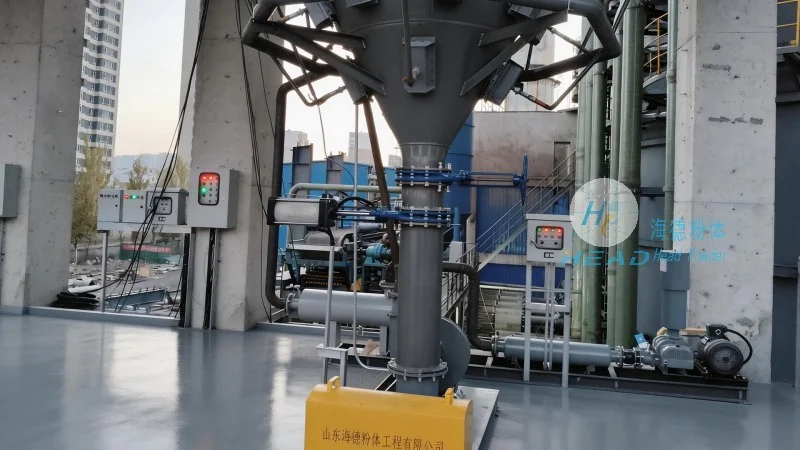
The core of a nitrile rubber pneumatic conveying system lies in its air-driven mechanism. The system typically consists of a hopper, a blower or air compressor, a pipeline network, and a receiver. The process begins when nitrile rubber is fed into the hopper. The blower then generates a high-velocity airflow that pulls the rubber particles into the pipeline. As the rubber travels through the pipeline, it is suspended and transported by the air stream. The receiver collects the material at the end of the pipeline, completing the conveying cycle. This air-driven method eliminates the need for mechanical components like belts or chains, reducing maintenance and increasing operational efficiency.

Key Features of Nitrile Rubber Pneumatic Conveying Systems
Several notable features distinguish nitrile rubber pneumatic conveying systems from traditional methods. Firstly, the systems offer high efficiency in material transport, capable of moving large volumes of nitrile rubber quickly and reliably. The air-driven design minimizes material degradation, as there is no direct contact with mechanical parts that could cause abrasion or wear. This is particularly important for nitrile rubber, which is sensitive to mechanical stress. Secondly, the systems provide excellent dust control. The enclosed pipeline and air filtration systems prevent dust from escaping into the environment, ensuring a clean and safe working environment. Additionally, the flexibility of the pipeline network allows for easy integration into existing production lines, adapting to various layout requirements. The systems also feature low energy consumption compared to other conveying methods, contributing to cost savings and environmental sustainability.
Application Benefits and Operational Advantages
Implementing a nitrile rubber pneumatic conveying system brings multiple benefits to industrial operations. The high transport efficiency reduces downtime and increases overall productivity. The reduced risk of material contamination and degradation ensures product quality consistency. The enclosed system design enhances workplace safety by minimizing exposure to dust and airborne particles. Furthermore, the modular nature of the system allows for scalability, enabling businesses to expand their conveying capabilities as production needs grow. The low maintenance requirements, due to the absence of moving parts, result in lower operational costs and less downtime for repairs. These advantages make nitrile rubber pneumatic conveying systems a preferred choice for industries handling nitrile rubber and similar materials.
Conclusion and Company Overview
Shandong HeadPowder Engineering Co., Ltd. is committed to delivering innovative and reliable nitrile rubber pneumatic conveying systems. With a focus on engineering excellence and customer satisfaction, the company provides tailored solutions that meet the specific needs of industrial clients. Based in Shandong, China, HeadPowder leverages its expertise to design and manufacture systems that enhance material handling efficiency while maintaining high standards of safety and environmental compliance. The company's dedication to quality and performance ensures that its clients receive robust, long-lasting equipment that supports their operational goals.